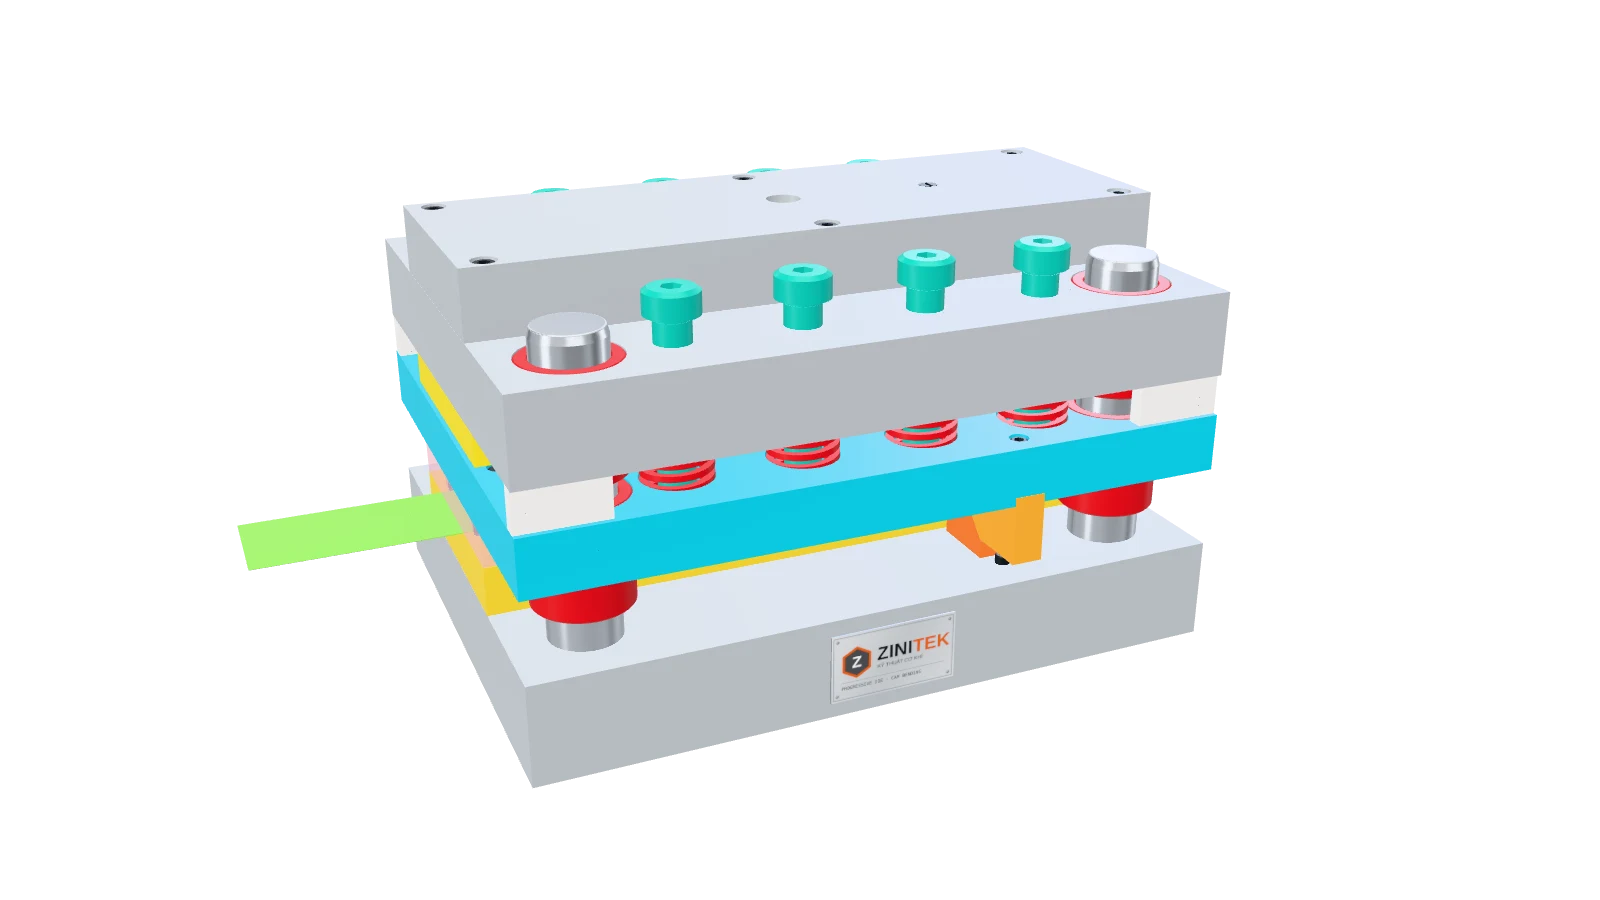
Progressive die for a metal clip with a side-acting cam: 0.4 mm strip, 59 mm wide, 22 mm pitch. Blanking, pilot piercing, multi-step bending, hook folding by a cam slide, wrap bending over a core and cut-off. The 3D model runs like a 30 spm crank press; rotate it right on this page.
Strip sequence: Ø3 pilot holes, blanking from both sides, rib and edge bending, 90° hook bend, hook folding by the side cam, U-wrap over a core, then cut-off; 7 pilots locate the 22 mm pitch.
Side-acting cam: a driver on the stripper pushes the slide in 5 mm just as the stripper clamps the strip and holds it while the punches continue down; a spring returns the slide as the die opens and a stop pin limits its travel.
The 3D model moves like a 30 spm crank press: the stripper clamps the strip, flanges bend gradually with the punch, cut scrap drops through the die and the shoe, and the finished clip is pushed off the die end.
Guided by 4 pillars Ø40 × 225 in bushes; with a 40 mm press stroke the pillars stay at least 36 mm inside the bushes; stop blocks limit the stripper travel to 14.4 mm.
Cutting and forming parts in SKD11 tool steel hardened to 58–62 HRC; shoes and holder plates in S50C to keep cost down; standard screws, dowels, pillars, bushes and springs.
Order to your drawing: send the part drawing, material and thickness, volume and press data, and ZINITEK will propose the strip layout and die design.
Progressive Die for Metal Clips with Cam Bending | ZINITEK
 Precision Mold Design & Manufacturing