15-Step Progressive Die with Spring Stripper and Pilots
Model: N/A
Tính năng nổi bật
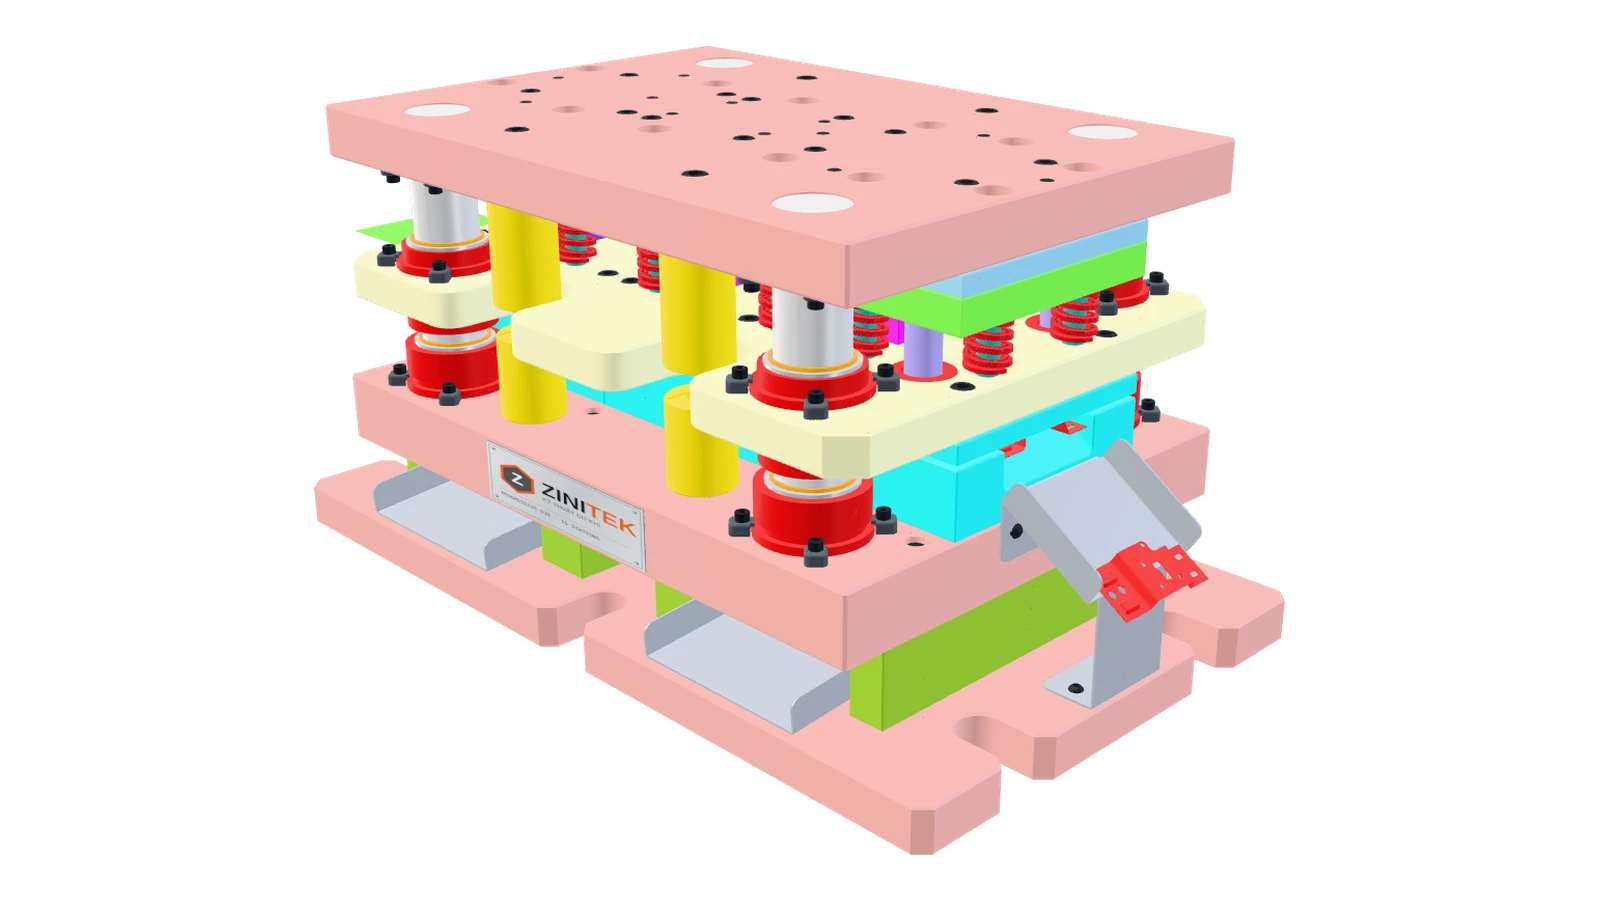
15-step progressive die with spring stripper and pilots for a 0.8 mm sheet-steel part: 114 mm strip, 45 mm pitch; piercing, blanking, a 13 mm deep Z-bend, a V-bend re-formed into a Z, embossing, ribbing and cut-off. Rotate the animated 3D model right on this page.
15 stations at a 45 mm pitch: pierce holes and pilot holes → blank the two wings → pierce the centre slot → 13 mm Z-bend on the right wing and V-bend on the left wing → re-form the V into a Z → pierce slots and holes and emboss → form ribs → cut off the part.
Spring-loaded pilots in the stripper re-locate the strip on every stroke; spring lifter rails at the entry raise the strip before each feed. The 3D model shows the die opening and closing, the bends forming gradually with the punches and the strip advancing one pitch per cycle.
A spring stripper clamps the strip flat before the punches cut and strips it off the punches as the die opens; slugs drop onto scrap chutes under the die shoe and the cut-off part slides out down the chute at the die end.
Guided by four Ø50 pillars with ball bushes; a press stroke of about 70 mm lets the strip with its deep bends feed, and the pillars still engage the bushes by about 26 mm at top dead centre.
Cutting and forming parts in SKD11 tool steel hardened to 58–62 HRC; shoes and holder plates in S50C to keep cost down; standard screws, dowels, pillars, bushes and springs.
Order to your drawing: send the part drawing, material and thickness, volume and press data, and ZINITEK will propose the strip layout and die design.
15-Step Progressive Die with Spring Stripper and Pilots | ZINITEK
 Precision Mold Design & Manufacturing