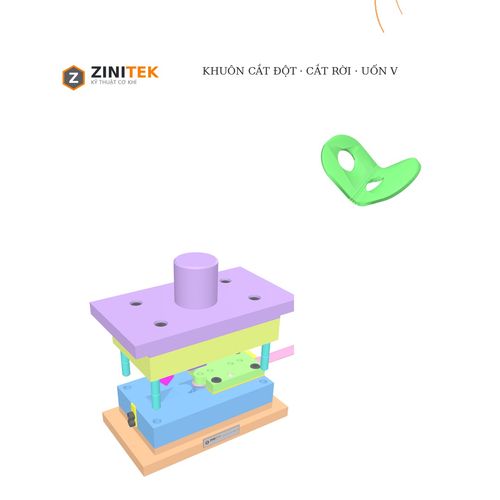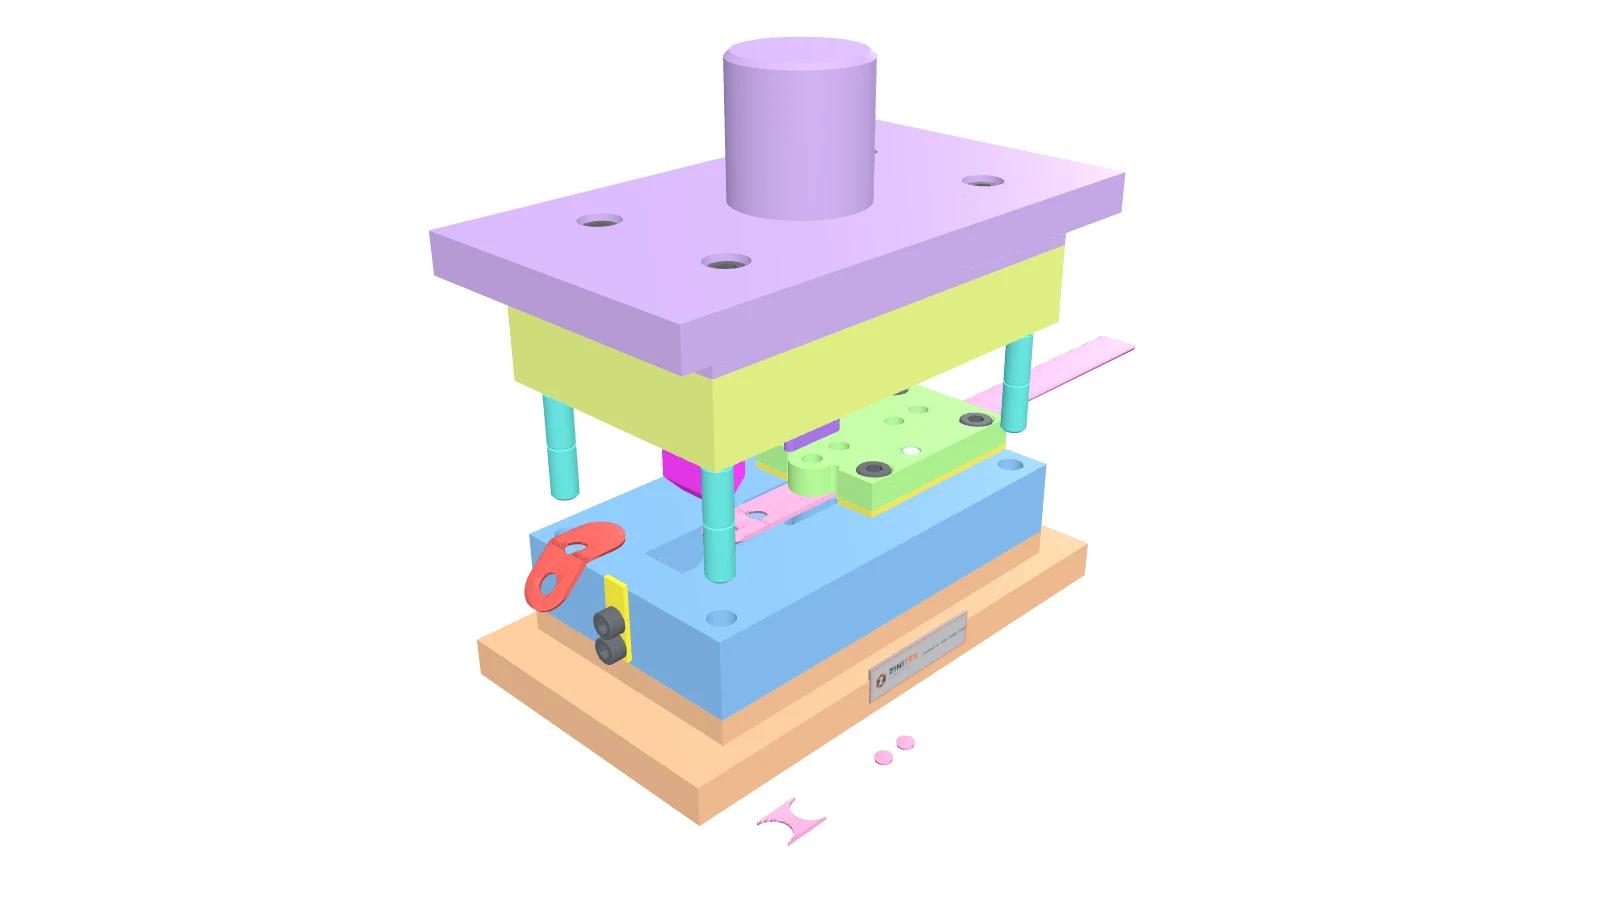
3D model
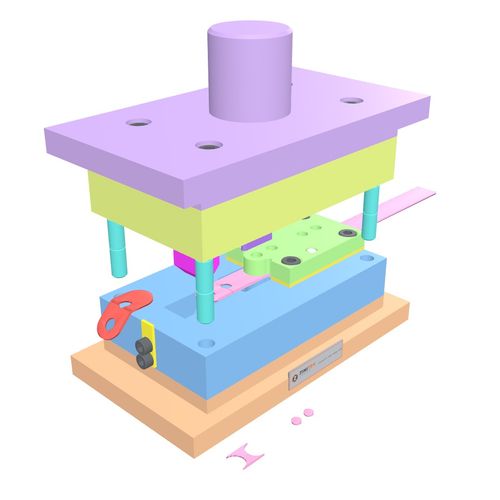
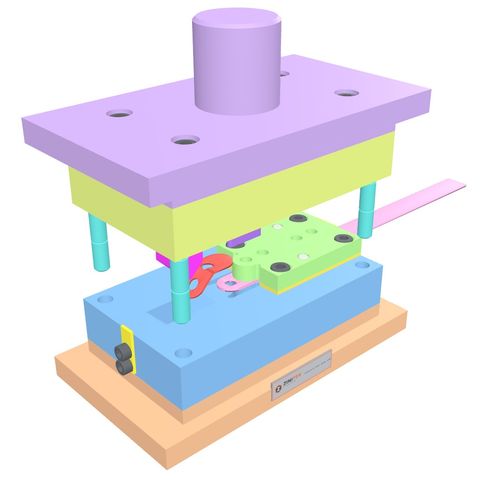
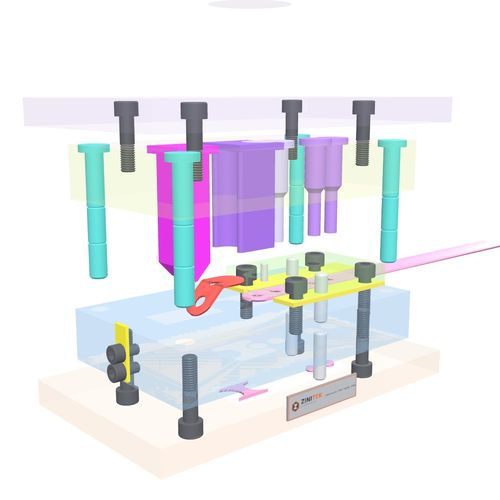
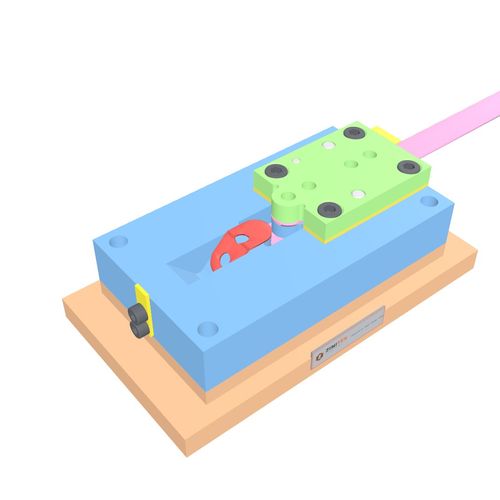
The view-only 3D model shows the complete die set: lower shoe and die block, fixed stripper with strip guides, punch plate and upper shoe, piercing punches, pilots, parting punch and V punch. It runs on a constant-speed crank at 40 strokes per minute with a 40 mm stroke: each stroke pierces two Ø8 holes, the pilots locate the pitch, the parting punch separates the link, slugs drop through the opening in the lower shoe and the strip advances 47 mm. The architecture view fades the plates so the punches, pins, threaded screws and the slug path can be seen.
Main structure
Die set 215 × 120 mm, shut height ≈ 186 mm, for an 18 × 2 mm strip at a 47 mm pitch. Four stations: two Ø8 holes 15 mm apart; two Ø8 pilots entering the pierced holes; an R9 double-arc parting punch producing the 18 × 42 round-ended link; a 90° V die 40 mm wide and 20 mm deep with an R1.2 V punch. The fixed stripper is held by 4 M8 screws and 2 Ø8 dowels; the upper shoe is bolted to the punch plate with 4 M8×30 screws; the die block is fastened from below with 4 M8×35 screws; 4 Ø10 centralizer pins locate the two halves on the down-stroke. Every component was identified and the whole cycle checked for collisions.
Engineering notes and improvement path
The original design is kept as it is for study. The V station sits only 2 mm from the parting line and is not on the pitch, so during the cutting stroke the V punch acts on the strip end overhanging the V die and the part has to be removed by hand; the model shows exactly this. For automatic production of the same part ZINITEK proposes a 6–7 station progressive die: part laid across a ≈ 52 mm strip with a one-side carrier at a 21 mm pitch; bend line parallel to the feed and a V groove running to the die edge so the part slides out by itself once its carrier tab is cut; spring stripper, 4 ball-cage guide pillars, SKD11 punches and dies at 58–62 HRC, S50C plates; a 25–35 t press with an NC feeder.
Discuss a die for your part
Send a drawing or reference sample with material, thickness, volume and press data and ZINITEK will discuss the design and manufacturing approach.
Project Gallery